Technical Overview of Mobile Concrete Batching Plant
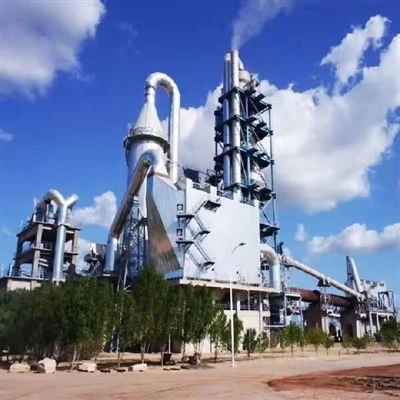
Mobile Concrete Batching Plant is defined as an integrated production unit. It combines aggregate batching, powder material storage and weighing, water and admixture supply, mixing unit, and control system on a towable chassis or containerized modules. Based on structural design, it is divided into two main types: semi-trailer type and containerized module type.


The key technical features of a mobile plant
Foundation-free or low-preparation ground operation
The plant carries its own support system during transport. By distributing the load, the ground bearing capacity requirement is reduced to below 1.5 MPa. No cast-in-place concrete foundation is required on site.
Hydraulic self-erecting mechanism
The cement silo and conveying system are raised from horizontal transport position to working position by the plant's own hydraulic cylinders. This operation is completed within 5 minutes. No external crane or lifting equipment is required.
Pre-wired electrical system
Control cables, sensor signal lines, and power cables are factory-installed inside conduits fixed to the chassis. On site, only 2 to 4 quick-connect cables and the main power supply line need to be connected.
On-Site Installation Procedure
Site Assessment and Preparation
Before the equipment arrives, a proper site assessment and necessary preparation are required. This ensures the mobile batching plant can be installed smoothly and operate stably.
Site Dimensions and Bearing Capacity Requirements
First, the site must be large enough to accommodate the fully expanded equipment. Generally, the effective site area should not be less than 1.2 times the projected area of the fully expanded plant. Additionally, a clearance of at least 1.5 m wide should be reserved around the equipment for daily operation and future maintenance access.
Second, ground levelness is also important. The ground slope of the entire working area should not exceed 3° (equivalent to a 5% gradient).
Third and most importantly, the ground must have sufficient firmness, which is referred to as bearing capacity. For a mobile batching plant, the required ground bearing capacity is not less than 1.5 MPa. If the native soil does not meet this requirement, two simple engineering solutions are available:
Lay a 200 mm thick layer of graded crushed stone with a particle size of 20–40 mm. After placement, compact the layer to achieve a minimum compaction degree of 93%.
Place 25 mm thick steel plates or dedicated load transfer pads directly under the equipment outriggers to distribute the load.

Drainage and Utility Connections
Site drainage must also be considered. To prevent water accumulation around the outriggers during rain, which could cause soil softening or uneven settlement, the installation ground should have a drainage slope of not less than 2‰. This allows rainwater to drain away naturally.
Next is power supply. The equipment voltage requirement depends on its nameplate. Two common types are 380–415 V / 50 Hz or 460 V / 60 Hz. The control panel requires a dedicated power circuit. To prevent tripping during equipment startup and operation, it is recommended to use a generator set with a capacity not less than 1.2 times the total equipment power. Based on experience, a 30–50 kVA generator is generally sufficient.
Finally, water supply for production is needed. The water source must provide a flow rate of at least 10 m³/h, and the inlet water pressure must be maintained between 0.2 and 0.4 MPa. This ensures normal production and cleaning of the batching plant.


Equipment Positioning and Mechanical Leveling
Chassis Positioning and Uncoupling
Use a tractor truck to tow the semi-trailer chassis to the designated position. First, disconnect the kingpin. Then, close the valves of the air brake system. Finally, place wheel chocks in front of and behind the tires to prevent unintended rolling.
Outrigger Extension and Leveling
First, extend the four hydraulic outriggers vertically downward until the tires are completely off the ground. The lift height should be controlled between 20 and 30 mm.
Next, use a frame spirit level or an electronic inclinometer to measure the levelness of the chassis in both the longitudinal and transverse directions.
Then, adjust the extension stroke of each outrigger based on the measurement results. Continue adjusting until the leveling error in both directions does not exceed 0.5 mm per meter (0.5 mm/m).
Critical Control Point: After leveling is completed, tighten the mechanical lock nut on each outrigger. This step is very important because the lock nuts bear the static load during long-term parking. They prevent the chassis from slowly settling due to minor internal leakage in the hydraulic cylinders.
Cement Silo Hydraulic Erection
Start the hydraulic power unit. Hydraulic oil drives the lift cylinders simultaneously through synchronizing valves. The cement silo begins to rise slowly from its horizontal position. The angular speed during this rotation should be controlled at no more than 3 degrees per second (≤3°/s).
When the cement silo approaches the vertical position (approximately 87°), manually fine-tune the alignment to precisely match the positioning pin holes on the silo base with the holes on the support bracket.
Continue lifting slowly until fully vertical. Then, manually insert two high-strength positioning pins. The pin diameter is typically 40 to 60 mm, and the material is 40Cr alloy steel or equivalent. After insertion, install cotter pins to prevent the positioning pins from loosening due to vibration.
Finally, relieve the pressure from the hydraulic cylinders. At this point, the full weight of the cement silo and its upper structure is completely carried by the positioning pins and the support bracket below. The hydraulic cylinders are no longer under load.

Mechanical and Piping Connections
After the main equipment is fully unfolded, the following mechanical connections must be completed
| Connection Location | Work Description | Tightening Torque Reference |
|---|---|---|
| Screw Conveyor | Connect the cement silo discharge outlet to the weighing hopper inlet. Use a clamp-type sealing gasket between the two flanges. | 350–400 N·m |
| Aggregate Conveyor Belt | Unfold the folded section, tension the conveyor belt, and adjust the anti-deviation idlers. | Not applicable (mechanical locking) |
| Water and Admixture Piping | Connect using quick-connect self-locking couplings. Verify that the sealing rings (EPDM or FKM material) are in good condition. | Hand-tighten plus locking clip |
| Compressed Air Piping | Connect the air compressor outlet to the air receiver tank and to the pneumatic butterfly valves. | Thread sealant + 40 N·m |
Electrical and Control System Connection
Main Power Supply Connection
Verify that the grid phase sequence matches the equipment requirements. Do not start any load before confirming the motor rotation direction.
Control Signal Connection
Insert the multi-core aviation plugs from the control cabinet into the corresponding sockets on the mixing unit, weighing system, and aggregate batching system.
Typical number of connections: 3 control cables + 1 load cell summing cable.
Grounding and Protection
The equipment chassis must be connected to a dedicated grounding electrode. The grounding resistance shall not exceed 4 Ω.

No-Load Commissioning and Calibration
- First, jog the screw conveyor motor. Check if the rotation direction matches the arrow mark on the housing.
- Then, jog the mixing unit motor. Confirm that the mixing arm rotation follows the direction shown on the nameplate. This is usually counterclockwise when viewed from above.
- If the rotation direction is wrong, swap any two phases at the power supply input side. Do not swap phases on the inverter output side.
- First, perform a tare calibration on each weighing hopper. Make sure the display shows zero when the hopper is empty.
- Then, perform a span calibration using the test weight method. Add known weights to each weighing hopper in sequence. Common test points are 20%, 50%, and 100% of the scale capacity. Record the sensor output values and calculate the linearity error.
- Calibration accuracy requirements: Dynamic weighing error ≤ ±1.0%. Static weighing error ≤ ±0.5%.
- Trigger each pneumatic butterfly valve and cylinder one by one. Check that they open and close fully without sticking or jamming.
- Finally, test the emergency stop button. After pressing the E-Stop button, all actuators must stop immediately.
Heavy-Load Test and Production Start Criteria
Washing the Mixer
Before the first batch of material, add clean water and a small amount of mortar into the mixing unit. Run the mixer for 2 to 3 minutes. This removes the anti-rust oil and welding slag from inside the mixer.
Trial Production
Continuously produce 3 to 5 batches of concrete according to the project mix design.
Inspection Criteria
- Slump: The deviation between the measured value and the design value shall not exceed 20 mm.
- Concrete Uniformity: According to ASTM C94 standards, sample the mortar and measure its density. The relative error of mortar density shall not exceed 0.8%.
Production Start Decision
The equipment can be formally put into production only after all the above criteria are met.
Reference Man-Hours
With one 5-ton forklift or loader available, two trained installation personnel can complete the entire process from equipment arrival to first batch discharge within 4 working hours.
Maintenance Technical Specifications
Maintenance for a mobile concrete batching plant is not complicated. The key is to follow a regular schedule. Below is a clear table showing what to check and how often.
Maintenance Schedule and Inspection Points
| Period | Main Inspection Area | Check Items and Standards |
|---|---|---|
| Daily | Mixer shaft seal lubrication | Check oil level in auto lubricator; interruption over 2 hours can damage bearings |
| Conveyor belt | Check misalignment (allow ≤5% of belt width), tears, and splice lifting | |
| Inside of mixer | After each batch, run with cleaning aggregate for 3–5 min, then high-pressure water rinse; clean material off discharge door seal | |
| Weekly | Mixing blades and liners | Measure gap with feeler gauge; allowable range: 3–8 mm; gap >10 mm reduces mixing efficiency by 15%–20% and may cause material buildup on shaft |
| Air system | Open drain valve at bottom of air receiver tank to remove condensate; water accumulation causes rust or ice blockage | |
| Load cells | Check for mechanical deformation; check cables for rodent damage or crushing | |
| Monthly | Structural connections | Use torque wrench to check mounting bolts on mixer vibration pads, silo locking pins, and outriggers; if torque loss >15%, re-tighten and apply thread locker (Loctite 243 grade) |
| Sensor accuracy | Recheck with known-weight bags of cement or sand; if error exceeds ±1%, re-calibrate | |
| Electrical cabinet | Blow out dust with dry compressed air (≤0.5 MPa); check relays and terminals for burn marks | |
| Quarterly | Screw conveyor flights | Remove end cover; measure gap between flight outer diameter and tube inner wall; if gap exceeds 1.5x original value, replace screw assembly |
| Gearbox oil | First change: after 500 hours; subsequent changes: every 2000 hours or 12 months (whichever comes first); recommended oil: ISO VG 220 synthetic gear oil | |
| Electrical insulation | Measure insulation resistance of motors and main cables to ground using 500V megger; value shall be ≥1 MΩ |
Recommended Spare Parts Stock
Based on a mobile batching plant with an annual output of 20,000 m³, the following consumable spare parts are recommended to be kept on site. Estimated budget: $1,500–$2,000 USD.
| Spare Part Name | Quantity | Purpose |
| Mixing arms / blades (one left, one right) | 1 set | Replace when wear exceeds limit |
| Liner plates (sector shape) | 2 pieces | Replace when wear exceeds limit |
| Load cell (same model) | 1 piece | Replace faulty load cell |
| Pneumatic butterfly valve seal ring | 2 sets | Fix air leakage or poor sealing |
| Conveyor belt cold repair strip | 1 roll | Emergency repair for local tears |
| Control relay and contactor auxiliary contacts | Several pieces | Electrical fault diagnosis and repair |
Typical Faults and Repair Measures
| Fault Phenomenon | Possible Cause | Inspection and Repair Procedure |
| Screw conveyor does not discharge material | Motor reverse rotation; cement caking inside the tube | Check phase sequence; Remove end cover and clear the caked material |
| Weighing value drifts | Load cell exposed to moisture; loose wiring | Check junction box seal; Measure load cell bridge resistance (350 ± 5 Ω is normal) |
| Unusual noise from mixer | Blades contacting liners; foreign metal object inside | Stop machine and check clearance; Open access door and remove foreign object |
| Discharge door does not close tightly | Worn seal ring; insufficient cylinder pressure | Replace seal ring; Check air supply pressure and cylinder seals |
Maintenance Cost of Mobile Concrete Batching Plant
Components of Maintenance Costs
The maintenance cost of a mobile concrete batching plant comes mainly from two parts: replacement of wear parts and labor for maintenance.
Unlike stationary plants, mobile plants are moved between job sites more often and have a compact design. As a result, wear is concentrated on a few high-load and high-frequency components.
According to industry data, for a mobile plant with an annual output of 20,000 m³, the material cost for consumable spare parts is approximately $300–$500 USD per 1,000 m³ of concrete produced. This cost does not include labor or downtime.
Among the material cost above, the three component systems with the highest shares are
Mixing arms and blades: About 40% of total maintenance material cost. These are the fastest-wearing parts because they directly bear the impact and friction of aggregates during mixing.
Conveyor belt and idlers: About 25%. Belt misalignment, tearing, and stuck idlers are the main reasons for replacement.
Pneumatic components and seals: About 15%. This includes cylinder seals, pneumatic butterfly valve seal rings, etc. They are affected by dust and moisture.
The remaining 20% is distributed among load cells, electrical contacts, lubricants, and other minor spare parts.
Spare Parts Budget
It is recommended to prepare a spare parts kit at the initial stage of plant operation. The budget for this kit is $1,500–$2,000 USD. The kit includes mixing arms, liner plates, a load cell, seal rings, belt repair strip, and relay contacts.
This stock can cover on-site replacement needs for about 3 to 6 months of normal operation. It helps avoid long downtime caused by waiting for spare parts delivery.


Installation Labor Cost Comparison
Compared with a stationary plant of the same capacity, a mobile plant saves significant labor cost during installation.
- Stationary plant installation labor: approximately $2,000–$4,000 USD
- Mobile plant installation labor: approximately $500–$1,000 USD
A mobile plant requires no concrete foundation, no steel structure platform, and no large crane. Two trained installers with one forklift or loader can complete the installation.
Key Points for Cost Control
- Perform daily shaft end lubrication checks. This prevents major repairs caused by bearing failure.
- Use a feeler gauge every week to check the gap between blades and liners. If the gap exceeds 10 mm, mixing efficiency drops by 15%–20%, and wear on other parts increases.
- Change the gearbox oil every quarter or every 2,000 operating hours (whichever comes first). This extends the life of the drive unit.